• Hi all and welcome to TheWoodHaven2 brought into the 21st Century, kicking and screaming! We all have Alasdair to thank for the vast bulk of the heavy lifting to get us here, no more so than me because he's taken away a huge burden of responsibility from my shoulders and brought us to this new shiny home, with all your previous content (hopefully) still intact! Please peruse and feed back. There is still plenty to do, like changing the colour scheme, adding the banner graphic, tweaking the odd setting here and there so I have added a new thread in the 'Technical Issues, Bugs and Feature Requests' forum for you to add any issues you find, any missing settings or just anything you'd like to see added/removed from the feature set that Xenforo offers. We will get to everything over the coming weeks so please be patient, but add anything at all to the thread I mention above and we promise to get to them over the next few days/weeks/months. In the meantime, please enjoy!

Spindle moulder shaft - 11/4 to 30mm?

Apparently all the spares for the SCM T120C are obsolete.

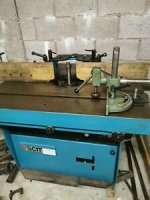
Spoke to a very nice chap from the saw centre, Glasgow, an ex-machinery engineer. He looked at the listing for me - bargepoles were nicely mentioned, at that price - and pointed out the original paint around the SCM label that dates it to late 70s. Someone’s done it up in tasteful Makita blue.
 

Attachments

  • 895236FF-C37B-4146-AAAD-391C749920AE.jpeg
    895236FF-C37B-4146-AAAD-391C749920AE.jpeg
    27.2 KB · Views: 7,671
Guineafowl21":2a8iz8p5 said:
Apparently all the spares for the SCM T120C are obsolete.

Spoke to a very nice chap from the saw centre, Glasgow, an ex-machinery engineer. He looked at the listing for me - bargepoles were nicely mentioned, at that price - and pointed out the original paint around the SCM label that dates it to late 70s. Someone’s done it up in tasteful Makita blue.

Wot? A man that buys a 90-year-old surface planer is scared of a ~40-year-old spindle moulder? :lol:

I would assume whoever's sticker that is next to the SCM badge is the one who painted it, doesn't look a terrible job though.

Good, unmolested machines are harder to come by more and more, take Wadkin AGS saws for example, you used to be able to pick these up for around £300 no problem a couple of years ago and now even a ratty one will fetch £1000, and there are loads of refurbished ones about of varying quality which don't seem to fetch as much as one that's in original work clothes.
 
Trevanion":adlp3lrc said:
Wot? A man that buys a 90-year-old surface planer is scared of a ~40-year-old spindle moulder? :lol:

I do love old sh1te, but at the right price!

Missing bits - table inserts, extraction outlet, Shaw guards, 30mm spindle = not worth £2k plus VAT plus delivery, I would humbly say.

I offered £1k, but was turned down. I do see the machinery man’s point, that it might end up not being a bargain after all the bits are bought/found for it.

Eyes still peeled.
 
Guineafowl21":3jv4xk91 said:
Missing bits - table inserts, extraction outlet, Shaw guards, 30mm spindle = not worth £2k plus VAT plus delivery, I would humbly say.

Ah, I missed that you mentioned that those bits were missing.

Like I mentioned, worth keeping an eye out on the other industrial auction sites as you can pick up a bargain, but there does tend to be a bit more rigmarole when it comes to decommissioning the machines on site, having to have a written risk assessment on how you plan on moving the machine, and in some cases needing a qualified electrician to unwire it. You also need to keep in mind the auctioneers fees, which add a lot onto the final price.

Here's a couple of examples:

https://www.bidspotter.co.uk/en-gb/...0475/lot-de87ff38-c55d-4ed1-9c2e-ad36010cbaba

https://www.bidspotter.co.uk/en-gb/...1078/lot-1dcc9bfa-95c6-449f-8369-ad320105c694

https://www.cottandco.com/en/lots/martin-t26-tilting-spindle-moulder-2005-
 
Aha! Trying to get me to buy a Martin now, are we? :shock:

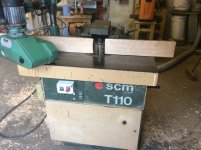
Still thinking about the T110 with the blurry pics. I bet I could do that up and shift it on.
 
Guineafowl21":31mec9b7 said:
Aha! Trying to get me to buy a Martin now, are we? :shock:

Why settle for anything else? :D

Guineafowl21":31mec9b7 said:
Still thinking about the T110 with the blurry pics. I bet I could do that up and shift it on.

I personally don't think you can go far wrong with the price so long as it's complete, perhaps put in a cheeky offer over message for less as it's not sold for the starting bid at least once. It clearly needs a bit of TLC, the SCM decal/plate looks like it's beginning to peel away but this could probably be stuck back and the switchgear looks like it could do with some attention. I reckon it's just dirty more than anything and it's a lot of machine for the money, the Maggi Steff powerfeeder unit would fetch £150-200 by itself every day of the week.
 
All that tooling, power feed and free delivery! Good deal.

The SCM 110 is on its way to me, or I might have gone for that.
 
Trevanion":11f3c7kd said:
Guineafowl21":11f3c7kd said:
All that tooling, power feed and free delivery! Good deal.

The SCM 110 is on its way to me, or I might have gone for that.

Why not both? :D
Get thee behind me, beelzebub :twisted:
 
Trevanion":3b9rz8d6 said:
Guineafowl21":3b9rz8d6 said:
Get thee behind me, beelzebub :twisted:

Well... If you do up the T110 to sell on... You're gonna need some form of replacement aren't ya? ;)
Er, thanks.

Might also be nice to walk into the shop without crowdsurfing over cast iron beds, no? :eusa-shifty:

I’m fairly dead set on eventually getting a machine with a flush sliding table - I don’t know how you mould end-grain without one (unless you are possessed by the spirit of Roy Sutton). Does the power feed help with this?

Tenoning is another one, although I’ve found no better machine for small runs and quick setup than the Wadkin BRA, even with the normal saw blade fitted. I do end up wearing most of the waste, though. I wondered if some door-type brush strip would help with that?
 
Guineafowl21":1whhecbn said:
I’m fairly dead set on eventually getting a machine with a flush sliding table - I don’t know how you mould end-grain without one (unless you are possessed by the spirit of Roy Sutton). Does the power feed help with this?

It depends. If you're doing fairly large panels for say a kitchen door, you shouldn't need a sliding table or really a power feeder (although a power feeder does make it much easier) as the risk of it dropping into the cutter apeture or breaking up during cutting is fairly slim, just start on the end grain first as you mould the panel and you will end up cutting with the grain on the last pass, so there won't be any break out. When you get into much narrower sections is when a sliding table does come into its own, although any number of jigs can be made up to suit the work.

A nice thing with a power feeder is that it enables you to take very light climb cuts with hardly any risk of the workpiece shooting off like an arrow (You do need fairly fresh rubbery rollers though, ancient crusty and glazed-over ones are a big no-no), so say you have a piece of timber that's particularly uncooperative when it comes to moulding, it may be advantageous to make a final skimming pass running the workpiece backward with the rotation of the cutter block rather than against it. This technique is also helpful when moulding end grain to prevent breakout as the cutter finishes its pass, for example, on a sliding sash window I will put seals on the top and bottom of the sashes, at the end of their cut the cutter will break out the end grain of the sash stiles, so before moulding it I will hold it firmly and pull the sash toward myself and with the rotation of the cutter for a couple of inches then pull it out and mould it the conventional way, this reduces the break out to almost nothing.

Guineafowl21":1whhecbn said:
Tenoning is another one, although I’ve found no better machine for small runs and quick setup than the Wadkin BRA, even with the normal saw blade fitted. I do end up wearing most of the waste, though. I wondered if some door-type brush strip would help with that?

They are a messy machine, particularly if you haven't got extraction hooked up. Most people will have a box fitted around where the blade comes to a rest and there will be an extraction port in this to catch the dust being shot backward. Also with the hole in the BRA's guard being pointed directly at the operator you do tend to get a good dusting, I've never seen anyone actually fit a hose to this but I can't see why you couldn't do it if you had a suitably sized flexy hose and an over-head rig of some kind to carry it, typically the hole just gets plugged or taped over.
 
The 110 arrived yesterday, and I’ve been giving it a rough clean up and general tinker - freeing up, missing bolts, etc. Note enormous cutter block:

22E04F2D-D5EF-4B5E-BCC9-EBB118CFDDAC.jpeg

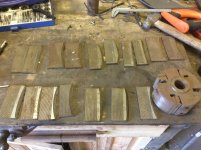
It came with some tooling, another cutter block, 40mm bore with top hats. It was from a cooper’s so I guess these are for shaping the staves:
9EE383DA-5677-498A-ADD1-CCD53ECB8138.jpeg

The motor is 5.5hp, 415V delta, and all that power is transferred with a tiny 8mm wide belt. It could do with a new one - is it a special type?

Steff 34 rollers could do with replacement. It’s been wired so that power is only available when the spindle’s running - this means I can’t set the roller height to clamp the wood, then shoot the piece out to start the spindle. Would it be more normal to be able to run the feed separately from the spindle?

Missing table inserts so I may have to make some out of plywood.

@Wallace could you put me in touch (or vice versa) with the man who can turn down the spindle?
 
Guineafowl21":1lmscfl6 said:
The 110 arrived yesterday, and I’ve been giving it a rough clean up and general tinker - freeing up, missing bolts, etc. Note enormous cutter block:

It came with some tooling, another cutter block, 40mm bore with top hats. It was from a cooper’s so I guess these are for shaping the staves

Ah, that already looks a bit better for a wipe-down and some less blurry photographs! :lol:

The cutter block that's on the spindle looks like a planing block of some kind? There are no scriber cutters on top from what I can see that would make it a rebating block. The cutter block with the cutters is a generic serrated type for use exclusively in four-sided planer moulders or CNC machines as there aren't any limiters, but so long as you look out the door and down the road each way for the Health and Safety officer before you load it in the machine and run it there shouldn't be any issues. Serrated knives tend to be twice as thick as the usual euro knives which means you can have a much greater maximum projection out of the cutter head without risk of it breaking during cutting.

Guineafowl21":1lmscfl6 said:
The motor is 5.5hp, 415V delta, and all that power is transferred with a tiny 8mm wide belt. It could do with a new one - is it a special type?

It's amazing, I accidentally ran a heavy window section through the spindle with a 9HP motor at the fastest speed on the power feed as we'd been doing half-lap cladding just before, didn't even flinch and all the power is also transmitted with the most piddly looking belt. I thought they would've used a PolyV at the very least on the spindle drive.

I don't think it will be a special kind of belt, there should be numbers on it that will tell you which one to get unless they've been rubbed off somehow. If you can't figure it out from anything on the belt you can always measure the thickness and width of the belt which will give you the profile and then you will need to wrap a string around the outside of the existing belt (or just cut it) and see what the overall outer length is and search for a belt that's the correct size. If all else fails you surely have somewhere local like an agricultural supplier that deals in belts and has a gizmo for measuring them?

Guineafowl21":1lmscfl6 said:
Steff 34 rollers could do with replacement. It’s been wired so that power is only available when the spindle’s running - this means I can’t set the roller height to clamp the wood, then shoot the piece out to start the spindle. Would it be more normal to be able to run the feed separately from the spindle?

The rollers are only about £10 each last I checked so they're not silly money to replace. Wiring it in-line is the norm for some reason, I've seen more machines where the power feed only comes on when the machine is running (on a star-delta machine it will start when the machine is switched to delta) than I have machines were you can run the feed independantly. To set the height I will just adjust it until the feed roller is just beginning to kiss the timber, pull the timber out, and then lower the feed by a full turn of the handwheel, the wheels are spring-loaded with quite a generous travel, although you don't want it set too tight as that will just stress it out.

This guy has a lot of table rings for sale from various machines, you might find something that fits but it won't be cheap: https://www.ebay.co.uk/sch/rodders818/m.html?_nkw=&_armrs=1&_ipg=&_from=

Alternatively, make your own from plywood or have an engineer turn some up for you.
 
Nice bit of kit!

I like to have separate control over the power feeder as I can do a test pass before actually cutting. Of course, sometimes that's not possible given cutter projection etc.
 
I think I’ll wire it up for independent feed - the only advantage of the other way is that the feed stops when the spindle stops, but I can live without that.

The cutter block fitted is 4” tall, and takes ages to spin down! Those large (7mm thick) serrated knives fit into that. HSE don’t come near here, but in any case I tend to use a false fence and now, the power feed (new rollers ordered), so no particular need for limiters. I might get a Whitehill combi block for it anyway.

I’ve seen those table rings - none of them big enough (270mm largest dia).

Have you ever noticed that Italian cars have the pedals very close together? I end up pushing two at a time - something to do with the Italian fashion for slim, pointy-toed shoes, apparently. With this machine, I find I struggle to get my workboot in to press the spindle lock :cry:
 
I’ve just noticed the 415V delta motor was running in star, meaning the machine would develop only 1/3 of the power and torque!

That means the 5.5hp machine is really giving out just under 2hp.
 
Guineafowl21":3frmo9zi said:
I’ve just noticed the 415V delta motor was running in star, meaning the machine would develop only 1/3 of the power and torque!

That means the 5.5hp machine is really giving out just under 2hp.

That might indicate a fault in the star delta controller that possibly was fitted originally and it might have been bypassed by someone?

5.5hp is just on the threshold of needing a gentle start to stop popping board fuses on startup.

Bob
 
Guineafowl21":qu6s2ikw said:
That means the 5.5hp machine is really giving out just under 2hp.

The beefiest 2hp spindle moulder in the land!

You both know more about how to solve that problem I ever will so I won't even comment :eusa-shifty:
 
I tried it DOL in delta and it spins up with gusto (I run a type D breaker, so no nuisance tripping nonsense), but seems to put quite a bit of strain on the belt. I’ve ordered a star delta rotary switch from RS - this will allow not only soft starting but let me select the low power option for ordinary work, putting less stress on the components.

I find the workpiece sometimes drifts away from the fence when using the power feed, despite slewing it inwards and applying plenty of pressure. This could be because the rollers are hard and crusty. Is it best to align the middle roller with the cutterblock, or have the feeder more towards infeed or outfeed?
 
Guineafowl21":164ep56z said:
I find the workpiece sometimes drifts away from the fence when using the power feed, despite slewing it inwards and applying plenty of pressure. This could be because the rollers are hard and crusty. Is it best to align the middle roller with the cutterblock, or have the feeder more towards infeed or outfeed?

They can be rather fickle to set up initially (and if you switch between feeding down onto the bed to feeding against the fence), I generally have it so that the centre-line of the shaft lines up with the space between the middle and rear wheel so that you can get the feed rollers closer without fouling the blades. It's also worth checking that all three rollers are fairly level with each other, they don't need to be absolutely spot on but you don't want it miles off either. You also want it to be relatively flat or ever so slightly tilted upwards towards the fence and downwards towards the operator, this way the rear edge of the roller has the most pressure and has a tendency to also creep the timber against the fence instead of it drifting away, again, you don't want to over-do it. You want a bit of lead towards the fence so that the timber is pushed up against it also.

New rollers will make a world of difference though.
 
As Trevion said.....one tip is to make sure the wheels are not shinny, I hold a piece of 40 grit on them whist spinning, roughing them up gives them grip again.

Sent from my Redmi Note 9S using Tapatalk
 
Heres a couple of contacts for the machine work. johnmillsne159hn@aol.com thats 'doubleboost'.
Another guy who would probably do it is Burt kwouk https://www.facebook.com/burt.kwouk1

I've been clearing loads of stuff from my workshop and found a pile of table rings. Most of them were for wadkin EQ but their is a couple of unknown ones. What size do you need. They werent daft money either at £25
 
wallace":3nsqcfjk said:
Heres a couple of contacts for the machine work. johnmillsne159hn@aol.com thats 'doubleboost'.
Another guy who would probably do it is Burt kwouk https://www.facebook.com/burt.kwouk1

I've been clearing loads of stuff from my workshop and found a pile of table rings. Most of them were for wadkin EQ but their is a couple of unknown ones. What size do you need. They werent daft money either at £25
Thanks. I must confess to being a typical miserable git in a shed, ie not on Facebook. I’ll try the first chap, and perhaps get the wife to message the other.

Table ring outer dia is 270mm, and I think the depth of the step is 10mm. Will confirm.

Update: New rollers have transformed the power feed. Star-delta switch fitted. Fences put over the planer to true up. I’m starting to like the machine too much to sell it. :eusa-doh:
 
Guineafowl21":38kiu4fw said:
Thanks. I must confess to being a typical miserable git in a shed, ie not on Facebook.

Join the club :lol:

Guineafowl21":38kiu4fw said:
Update: New rollers have transformed the power feed. Star-delta switch fitted. Fences put over the planer to true up. I’m starting to like the machine too much to sell it. :eusa-doh:

I told you they would! If you were a proper cheapskate and had access to a lathe you could do this:

WU88V8x.png

UTVgkon.png

zPeANC8.png

titwIRh.png
 
Funny you should say that, *ahem* the reason I bought new ones is that the old wheels wouldn’t fit in my mate’s wood lathe chuck :eusa-whistle:

I’ve no strong objection to Facebook, but when I was on it, I was constantly stopping what I was doing to retrieve a message, only to find the announcement was - ‘your sister-in-law has posted a picture of her breakfast’.

Now, you can turn these things off, I know, but I swear they kept turning themselves back on again. I’d had enough of stopping the tractor/machine/car for inanities, and so returned to the bosom of grumpygittery.
 
Thanks Wallace, John Mills is looking at the spindle job for me.

It pops nicely off a taper by way of a jack nut:

F1F62A53-D39E-4152-9DC8-BB1FE9D9D4EA.jpeg

He got me to scrape a file across to assess the hardness. A couple of questions:

1. What dimension are we aiming for? I’d guess 30.00mm then sand back to an easy sliding fit, for which I’ll send on a 30mm spacer.

2. It’s drilled and tapped at the top, I think for a stabilising bearing for extra heavy work. Could I use an ordinary bolt and clamp washer, or should he make a new nut, 30mm by whatever pitch is already there?

3. I’ve got a DC brake ordered - would it be wise to use a locking spacer underneath whatever clamp we decide on? I was thinking a spacer with a roll pin that engages the vertical slots.
 
Guineafowl21":1p9q14h0 said:
1. What dimension are we aiming for? I’d guess 30.00mm then sand back to an easy sliding fit, for which I’ll send on a 30mm spacer.

I measured the shaft of my Sedgwick the other day, funnily enough, it was 29.90mm. I'll measure a couple more machines and see what it is across the board.

Guineafowl21":1p9q14h0 said:
2. It’s drilled and tapped at the top, I think for a stabilising bearing for extra heavy work. Could I use an ordinary bolt and clamp washer, or should he make a new nut, 30mm by whatever pitch is already there?

3. I’ve got a DC brake ordered - would it be wise to use a locking spacer underneath whatever clamp we decide on? I was thinking a spacer with a roll pin that engages the vertical slots.

I'd be tempted to completely cut off the threaded portion of the shaft, which should leave you a usable length of ~125mm which is more than enough height for any block you're going to be putting on a 30mm spindle, drill and tap for an M16 thread about 50mm of depth, and then copy the modern SCM shaft tops, like the ones I made the other day:

Nuaa3hg.png

d2hqOqK.png

KdYIBxy.png

The two lugs that project out of the "nuts" engage with an identically sized slot cut into the top of the shaft, which answers the braking problem, much simpler to make than making a nut and re-cutting the thread on the shaft.
 
Thanks - I’ll put that to him. Making up those spacers might make a fun video. You must have had fun making those!
 
So I’ve measured a few more shafts (6 in all!) with a micrometer, the Sedgwick SM3 and GW seem to be 29.90mm while the SM4II is 30mm exactly, the SCM and Felder moulders are also 30mm exactly. I suspect the SCM and Felder ones are cylindrically ground for high accuracy but a turned spindle should be accurate enough.
 
Trevanion":3np60hr7 said:
So I’ve measured a few more shafts (6 in all!) with a micrometer, the Sedgwick SM3 and GW seem to be 29.90mm while the SM4II is 30mm exactly, the SCM and Felder moulders are also 30mm exactly. I suspect the SCM and Felder ones are cylindrically ground for high accuracy but a turned spindle should be accurate enough.
Thanks. You have 6 spindle moulders?!

Update - I’m just waiting to post the spindle off to John Mills (watched a few of his videos, now refer to every awkward occurrence as BASS-TAD!) - the chap at the Saw Centre Glasgow says he might have a 30mm SCM shaft for a reasonable price, but of course has not rung me back.
 
I get to play with a lot of nice toys 8-)

So here's what the caps look like in the SCM when they're in the shaft, just to illustrate what I was trying to explain:

2u9qajV.png

This is a standard shaft (I think a 150mm or longer shaft was an optional extra), it's 130mm from base to the very top:

ONEcncO.png

On the other SCM machine it's a little different as it's a screwthread like yours with two keyways down the shaft:

I4G1JIk.png

The nut has a strange little captive washer of some kind incorporated into the nut which is able to rotate freely until it's locked into the keyways with the two lugs inside. I guess once it's locked into the keyways it means the inertia of the brake can't undo the washer that's bearing on the spindle spacers and prevents the nut from becoming undone:

mC7QwjZ.png
 
What do we think of this one?

https://www.gumtree.com/p/other-power-t ... 1405870951

The SCM is all ready to go - everything works and is cleaned up, Crompton DC brake fitted, spindle pending a change to 30mm (may not bother). @Trevanion, fancy a lucky 7th spindle moulder? :mrgreen:

If the power feed would swap over to the Startrite, that would be ideal. I have a nice bit of 10mm steel plate for extra support if needed.
 
Guineafowl21":2li0ofrd said:
What do we think of this one?

I've never seen one of those :eusa-think:

And googling it doesn't bring up too many results either so obviously not too many were made, there's been a few sales of them on Bidspotter and such where they've fetched about £650 with all the bells and whistles like your example. I did find this advertorial image though:

startrite-t160-txt.jpg


Doesn't look like a bad machine, although I would've expected a 4hp motor rather than 3hp, which is fine but will struggle on heavier cuts. It's a step-up from the Charnwood but quite a step-down from the SCM, its only real merit is the sliding table.

Guineafowl21":2li0ofrd said:
spindle pending a change to 30mm (may not bother). @

I'd still do it even if you plan on selling the machine, a machine with a 30mm spindle is far more desirable than one that's 1 1/4" and will sell much better.
 
Ta - I might have a look at it. For not much money I could fit a 4hp motor. This one’s three phase, which is I think a ‘better’ 3hp than single phase.

Do you think it would take the Steff 34 power feed?
 
Guineafowl21":er07q9g2 said:
Do you think it would take the Steff 34 power feed?

I can't think of a reason why it shouldn't, should be a case of drilling four holes in the bed and bolting it to it.
 
Ok, well there is a Sedgwick SM4 with sliding table on sale not a million miles from you - Barry somewhere. Well over budget but they might take a part exchange with my two machines.

Otherwise I’ll end up with three spindle moulders, ie halfway to your level of madness... :eusa-snooty: :mrgreen:
 
Guineafowl21":2b9mb5et said:
Ok, well there is a Sedgwick SM4 with sliding table on sale not a million miles from you - Barry somewhere. Well over budget but they might take a part exchange with my two machines.

Otherwise I’ll end up with three spindle moulders, ie halfway to your level of madness... :eusa-snooty: :mrgreen:

The one that Trebor has up on their website? Quite pricey, especially when we were only looking to buy a router table to begin with :lol:

Trebor has probably had it in stock for years much like the rest of their equipment, they are very expensive on the secondhand gear. They also have a integral sliding table SCM of the same vintage as yours for sale for less than the Sedgwick (which is expensive because it's single-phase, probably adds £1000 onto the price in Trebor's mind):

http://www.treborwoodworkingmachine...ge=product_info&cPath=63_74_9&products_id=341

Generally, the part-ex rate with woodworking machinery dealers is absolutely shocking, worse than cars. So if you can I think it would be better to sell them privately if you do consider it.
 
Trebor, yes!. It IS a bit pricey - I phoned up, got a deaf old boy with his telly in the background. Told to phone back when ‘Nicky’ is back from picking up the kids.

Phoned a couple more times, she wasn’t there, so I left my number with him so ‘she can call me when she gets in the door’. Heard nothing. Seems a bit Mickey Mouse to me.
 
Back
Top